Description
1. Product Overview
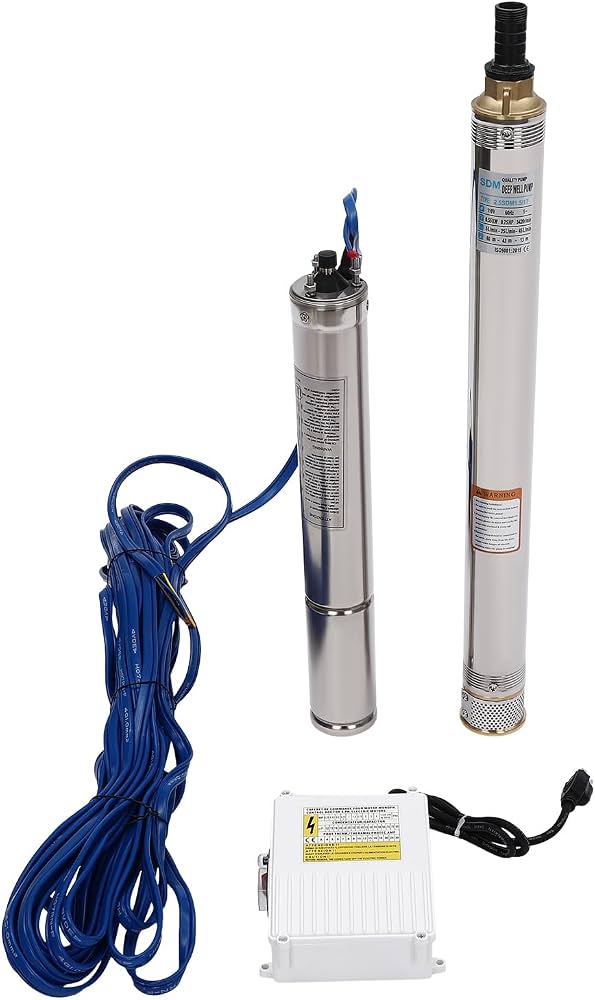
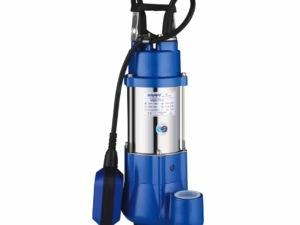
The 1HP Export Grade Submersible Pump is a high-performance water pumping solution engineered for efficient water extraction and transfer in residential, agricultural, commercial, and light industrial applications. Designed for submerged operation, it delivers reliable pumping performance for boreholes, wells, water tanks, irrigation systems, and general water supply. Its durable construction, efficient motor, and dependable hydraulic performance support consistent operation while reducing maintenance requirements. It is a strategic choice for buyers seeking reliable water management equipment for domestic, agricultural, and infrastructure projects.
2. Key Specifications & Technical Characteristics
-
Product Type: Submersible Water Pump
-
Power Rating: 1HP (0.75kW)
-
Grade: Export Grade
-
Motor Type: Electric submersible motor
-
Pump Construction: Corrosion-resistant metal components
-
Pump Housing: Stainless steel or cast iron, depending on configuration
-
Impeller Material: Stainless steel or engineering polymer, depending on model
-
Operating Principle: Centrifugal water pumping
-
Power Supply: Available in single-phase configurations; voltage options subject to specification
-
Physical Characteristics: Compact, sealed, water-resistant design
-
Installation: Vertical submerged installation
-
Packaging: Export-standard protective carton or wooden crate packaging
-
Shelf Life: No fixed shelf life under appropriate storage conditions
-
Origin: Subject to manufacturer and supplier specification
3. Core Industrial Applications
-
Agriculture and Irrigation: Water extraction from wells and boreholes for crop irrigation and livestock supply.
-
Residential Water Supply: Pumping water into overhead tanks, storage reservoirs, and domestic distribution systems.
-
Construction: Water transfer and drainage for construction sites and infrastructure projects.
-
Commercial Facilities: Water supply for hotels, institutions, warehouses, and commercial buildings.
-
Water Management: Transfer of clean water between storage tanks, reservoirs, and distribution networks.
Its submerged operating design eliminates the need for conventional surface priming, supports space-efficient installation, and provides dependable water delivery for suitable pumping depths and flow requirements.
4. Competitive Advantages
-
Quality Consistency: Export-grade construction designed for dependable performance and consistent manufacturing standards.
-
Supply Reliability: Suitable for bulk procurement, wholesale distribution, and recurring project requirements.
-
Operational Efficiency: Efficient 1HP motor configuration supports practical water pumping requirements.
-
Durability: Robust pump components help withstand regular operation under appropriate installation and maintenance conditions.
-
Logistics Capability: Export-ready packaging supports international shipping and bulk distribution.
-
Price Competitiveness: Cost-effective solution for distributors, contractors, agricultural operators, and institutional buyers.
-
Technical Documentation: Product specifications, installation guidance, and manufacturer documentation available subject to supplier provision.
5. Commercial & Supply Information
-
Minimum Order Quantity (MOQ): Bulk – 20 MT
-
Loading Capacity: Subject to pump dimensions, packaging configuration, and container type.
-
Container Options: 20ft and 40ft containers.
-
Supply Arrangement: Bulk wholesale and export supply.
-
Packaging: Export-standard protective packaging suitable for international transportation.


Reviews
There are no reviews yet.