Description
1. Product Overview
Nattokinase Enzyme Powder (NK-20000 FU) is a high-activity enzyme preparation standardized to approximately 20,000 fibrinolytic units (FU) per specified dosage or production standard, depending on the supplier’s assay method. It is primarily used as a functional ingredient in nutraceuticals, dietary supplements, and specialized enzyme formulations. Its high activity concentration enables formulators to achieve targeted enzyme potency with efficient dosage control and streamlined formulation design. As demand for enzyme-based functional ingredients expands globally, consistent activity, traceability, and reliable bulk supply make this product a strategic sourcing option for supplement manufacturers.
2. Key Specifications & Technical Characteristics
- Product: Nattokinase Enzyme Powder
- Activity Grade: NK-20000 FU
- Active Component: Nattokinase enzyme derived from fermented Bacillus subtilis natto
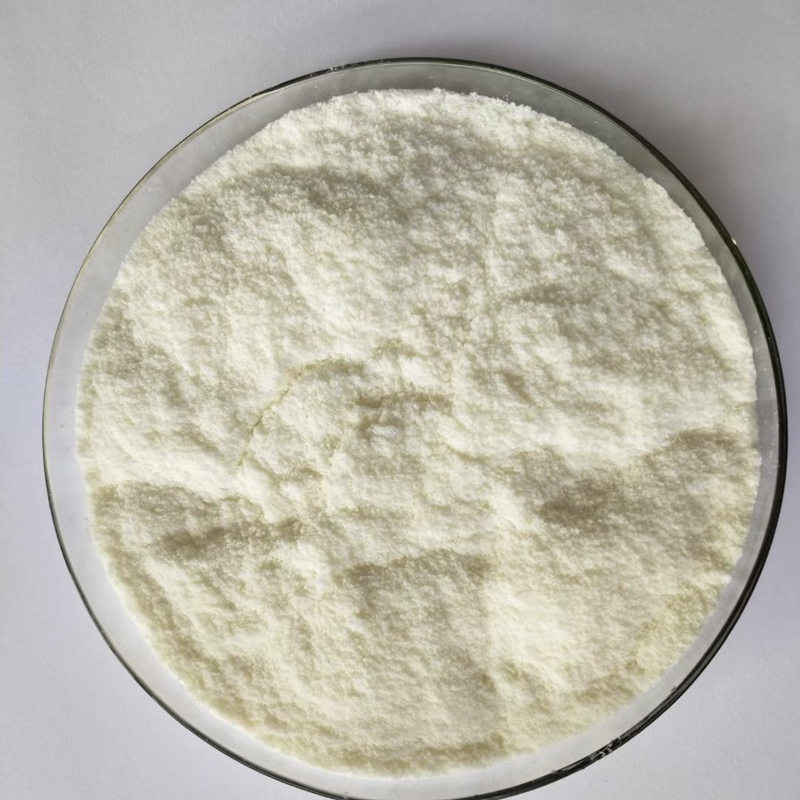
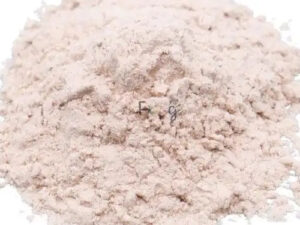
- Form: Fine powder
- Color: Typically off-white to light yellow/brown, depending on processing and carrier system
- Activity Assay: Fibrinolytic activity expressed in FU; specification should be verified against the supplier’s validated assay method
- Purity/Grade: Food-grade or nutraceutical-grade, subject to supplier specification and regulatory requirements
- Particle Size: Supplier-controlled powder specification; customizable screening may be available
- Moisture: Controlled according to applicable product specification
- Packaging Options: 1 kg, 5 kg, 10 kg, 20 kg, 25 kg bags/drums, or customized bulk packaging
- Storage: Store sealed in a cool, dry environment away from heat, moisture, and direct sunlight
- Shelf Life: Typically 24 months under recommended storage conditions, subject to manufacturer specification
- Documentation: COA, SDS, technical data sheet, batch/lot traceability, and applicable food/nutraceutical compliance documentation available according to supply program
3. Core Industrial Applications
- Nutraceutical Manufacturing: Used as an active enzyme ingredient in capsules, tablets, powders, and functional formulations.
- Dietary Supplements: Suitable for manufacturers developing enzyme-based wellness and functional supplement products.
- Functional Food Formulation: Can be incorporated into selected functional food and beverage systems where enzyme activity and processing compatibility are appropriate.
- Private-Label Production: Supports contract manufacturers requiring standardized enzyme activity for branded supplement programs.
- Bulk Ingredient Blending: High activity concentration facilitates controlled incorporation into premixes and multi-ingredient formulations.
The principal commercial advantage is activity standardization, allowing manufacturers to formulate according to measurable enzyme potency rather than relying solely on raw-material weight. Consistent batch activity, controlled moisture, appropriate packaging, and validated analytical documentation can improve formulation reproducibility and reduce quality-control variability.
4. Competitive Advantages
- Quality Consistency: Standardized enzyme activity supports repeatable formulation performance and batch-to-batch control.
- Supply Reliability: Structured bulk production and standardized packaging support continuous procurement programs for industrial manufacturers.
- Logistics Capability: Available in export-oriented packaging configurations with documentation suitable for international B2B shipment.
- Price Competitiveness: Bulk procurement and larger-volume supply programs can improve landed-cost efficiency for high-volume supplement manufacturers.
- Product Stability: Controlled moisture and protective packaging help preserve enzyme quality throughout appropriate storage and handling conditions.
- Technical Documentation: COA, SDS, specifications, assay information, and batch traceability can support buyer qualification and quality-assurance processes.
- Strategic Sourcing Value: A standardized high-activity enzyme ingredient can help manufacturers optimize dosage, simplify procurement, and maintain consistent finished-product specifications.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20 MT per container, subject to packaging configuration, container payload restrictions, and destination requirements
- Supply Format: Bulk industrial supply with customized packaging and documentation available upon commercial agreement
Reviews
There are no reviews yet.