Description
1. Product Overview
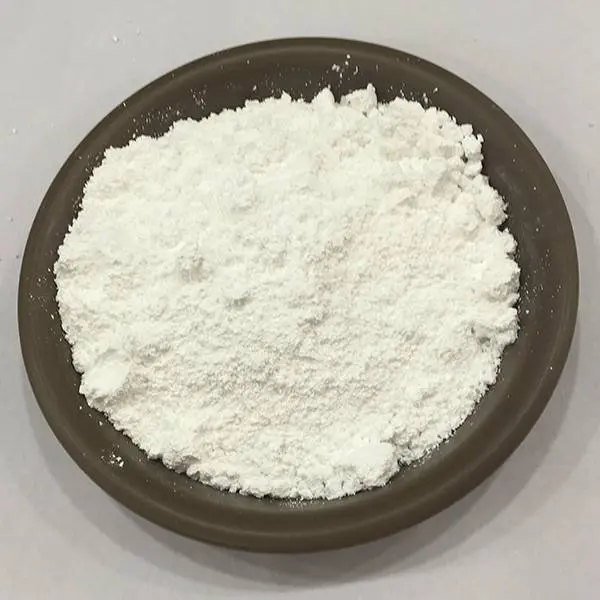
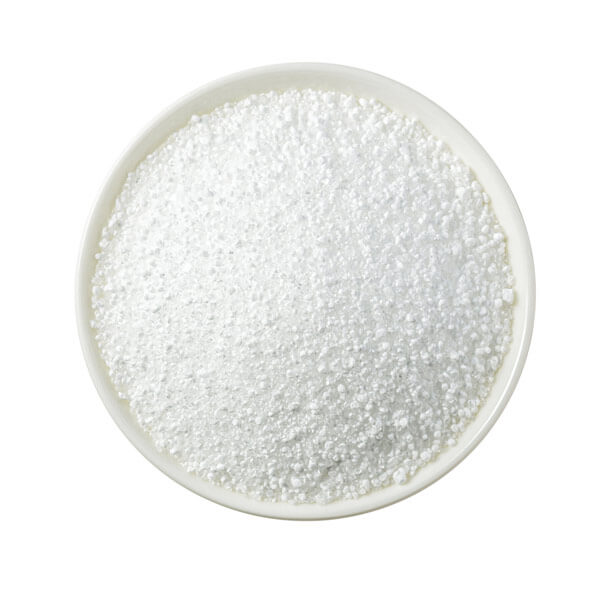
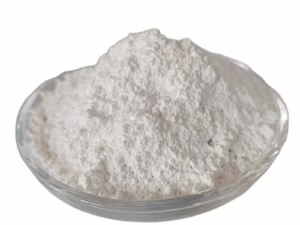
High Purity Alumina Nano Powder (HPA-99.99) is a 99.99% purity aluminum oxide (Al₂O₃) engineered in fine nano-scale powder form for demanding advanced-material and high-performance industrial applications. Its exceptional chemical purity, thermal stability, hardness, electrical insulation, and controlled particle characteristics make it suitable for technical ceramics, electronics, battery materials, optical components, and specialty coatings. HPA-99.99 enables manufacturers to achieve superior material performance while minimizing contamination from trace impurities. As demand grows for high-performance ceramics, energy-storage technologies, and advanced electronic materials, high-purity alumina is a strategically important material for next-generation manufacturing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Aluminum Oxide (Al₂O₃)
- Purity Level: ≥99.99% HPA grade
- Form: Fine nano-scale powder
- Color: White
- Particle Size: Nano-scale; typically controlled according to application requirements
- Crystal Structure: α-Al₂O₃ or other specified phase depending on application and processing requirements
- Thermal Stability: Excellent high-temperature stability and resistance to thermal degradation
- Hardness: Very high, providing excellent wear and abrasion resistance
- Electrical Properties: High electrical insulation capability
- Chemical Resistance: Strong resistance to corrosion and chemical attack
- Density: True density typically around 3.9–4.0 g/cm³; bulk density varies with particle morphology and packing
- Packaging Options: 20–25 kg moisture-resistant bags, fiber drums, or customized industrial bulk packaging
- Shelf Life: Typically 24 months when stored sealed in a dry, clean environment
- Storage: Keep tightly sealed and protected from moisture, contamination, and excessive heat
3. Core Industrial Applications
- Advanced Ceramics: Used in high-performance ceramic components, substrates, wear parts, cutting materials, and precision engineering components where high hardness and thermal stability are required.
- Electronics & Semiconductor Manufacturing: Suitable for electronic substrates, insulating components, thermal-management materials, and specialty ceramic parts requiring extremely low impurity levels.
- Battery & Energy Storage: Used as a high-purity ceramic and functional-material component in selected lithium-ion battery and next-generation energy-storage applications.
- Optical & Sapphire Materials: High-purity alumina serves as a critical feedstock for sapphire production and other transparent or specialty ceramic materials.
- Thermal Management: Used in electrically insulating, thermally conductive materials and ceramic fillers designed for demanding heat-management applications.
- Protective Coatings: Incorporated into wear-resistant, abrasion-resistant, and chemically resistant surface coatings.
- Catalyst & Specialty Materials: Applicable as a high-purity ceramic precursor, catalyst support material, and functional additive where contamination control is critical.
Its combination of ultra-high purity, controlled particle characteristics, thermal stability, and mechanical performance can deliver greater consistency and durability than conventional lower-purity alumina grades, particularly in precision applications where trace contaminants can compromise final-product performance.
4. Competitive Advantages
- Quality Consistency: 99.99% purity with controlled particle characteristics supports repeatable processing and reliable finished-product performance.
- Supply Reliability: Structured bulk supply programs support continuous industrial production and long-term sourcing requirements.
- Logistics Capability: Available in export-ready industrial packaging with bulk-order coordination and containerized shipment planning.
- Price Competitiveness: Bulk procurement and scalable supply arrangements help optimize total material cost for high-volume manufacturers.
- Performance Advantage: Excellent hardness, thermal stability, electrical insulation, and chemical resistance support demanding high-performance applications.
- Sustainability: Long service life and durable ceramic performance can contribute to reduced replacement frequency and improved material efficiency.
- Technical Documentation: Product specifications, certificate of analysis (COA), safety documentation, and technical data can be provided subject to order and application requirements.
- Strategic Sourcing Value: HPA-99.99 provides manufacturers with a dependable high-purity feedstock for advanced ceramics, electronics, energy-storage, and specialty-material production, supporting quality control and scalable manufacturing.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20 MT per 20-foot container, subject to packaging configuration, applicable payload restrictions, and shipping requirements
- Supply Format: Bulk industrial supply with customized packaging and shipment arrangements available for qualified buyers
Reviews
There are no reviews yet.