Description
1. Product Overview
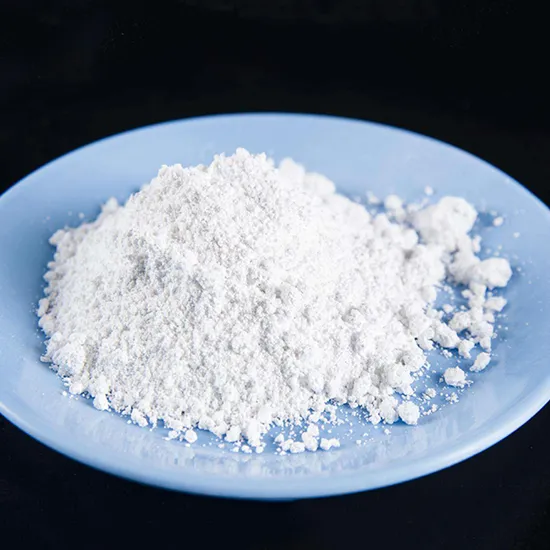
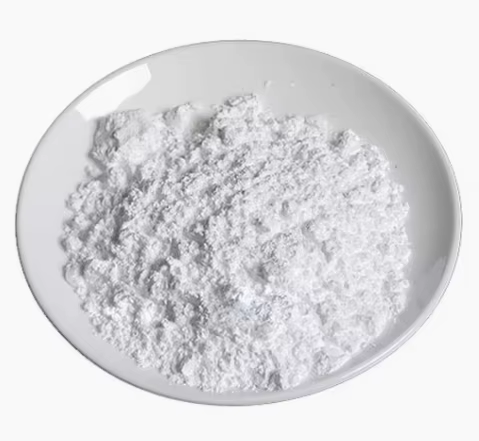
Hafnium Oxide Powder (HfO₂-99.9) is a high-purity advanced ceramic material valued for its exceptional thermal stability, chemical resistance, and electrical insulation properties. It is primarily used in high-performance ceramics, refractory materials, optical coatings, semiconductor-related applications, and specialized electronic components. With 99.9% purity, the material supports demanding applications where controlled composition and reliable performance are critical. Its combination of high-temperature durability and functional stability makes it a strategically important material for advanced manufacturing and high-value technology supply chains.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Hafnium Oxide (HfO₂)
- Purity: ≥99.9%
- Grade: Industrial / Advanced Materials Grade
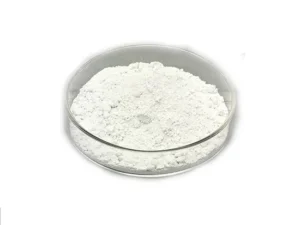
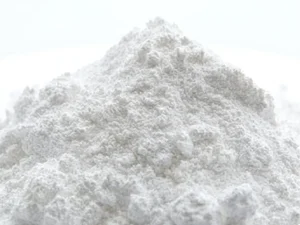
- Form: Fine powder
- Color: White to off-white
- Thermal Characteristics: High melting point and excellent high-temperature stability
- Chemical Characteristics: Strong resistance to corrosion and chemical degradation
- Electrical Properties: High dielectric strength and electrical insulation capability
- Particle Size: Customizable according to application and buyer specification
- Packaging Options: 1 kg, 5 kg, 25 kg bags/drums; bulk packaging available for industrial orders
- Shelf Life: Typically 24 months when stored sealed in a dry, cool environment
- Documentation: Certificate of Analysis (CoA), Safety Data Sheet (SDS), and technical specifications available upon request
3. Core Industrial Applications
- Advanced Ceramics: Used in high-performance ceramic components requiring exceptional thermal and chemical stability.
- Refractory Materials: Supports furnace linings, thermal components, and other high-temperature applications.
- Semiconductor & Electronics: Utilized as a high-k dielectric material and in specialized electronic and thin-film technologies.
- Optical Coatings: Applied in protective and functional coatings where high refractive index and durability are required.
- Aerospace & High-Temperature Engineering: Suitable for specialized components exposed to extreme thermal and chemical environments.
- Research & Advanced Materials: Used as a precursor for hafnium-based compounds, engineered ceramics, and emerging functional materials.
4. Competitive Advantages
- Quality Consistency: 99.9% purity supports controlled processing and reproducible industrial performance.
- Supply Reliability: Bulk sourcing programs can support continuous manufacturing requirements and long-term procurement.
- Logistics Capability: Flexible packaging and bulk shipment options facilitate international industrial supply.
- Price Competitiveness: Scalable sourcing and bulk-volume procurement provide opportunities for optimized landed cost.
- Performance Advantage: Excellent thermal stability, chemical resistance, and dielectric properties support demanding applications where conventional oxides may be insufficient.
- Sustainability: Long service life and high-performance characteristics can reduce material replacement and maintenance requirements.
- Technical Support: Product specifications, CoA, SDS, and application-related technical documentation can support qualification and procurement processes.
- Strategic Sourcing Value: A reliable supply of high-purity HfO₂ helps manufacturers secure a critical advanced-material input while maintaining quality and production continuity.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20 MT per 20-foot container, subject to packaging configuration, container payload limits, and applicable shipping regulations
Reviews
There are no reviews yet.