Description
1. Product Overview
Brown Rice Protein Concentrate is a high-quality plant-based protein ingredient produced from whole brown rice through advanced milling and protein concentration processes. It is widely used in the food, beverage, nutraceutical, sports nutrition, and functional ingredient industries due to its balanced nutritional profile, excellent digestibility, and clean-label appeal. This protein concentrate delivers a reliable source of plant protein for manufacturers seeking allergen-friendly and vegan formulations while maintaining consistent product performance. As global demand for sustainable plant-based ingredients continues to grow, Brown Rice Protein Concentrate has become a strategically important raw material for innovative product development and large-scale food manufacturing.
2. Key Specifications & Technical Characteristics
- Composition: Concentrated brown rice protein with naturally occurring amino acids and carbohydrates
- Protein Content: Typically 70–80% (food grade, depending on specification)
- Grade: Food Grade / Nutraceutical Grade
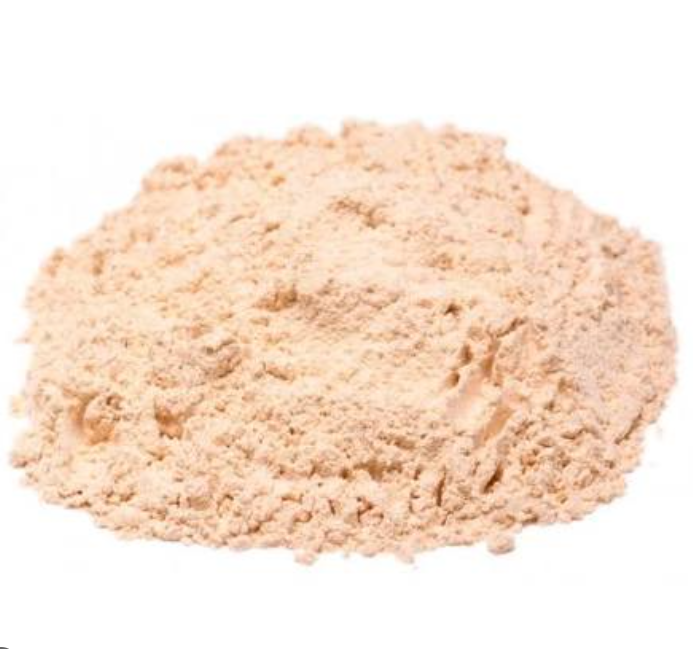
- Appearance: Fine, free-flowing powder
- Color: Light beige to cream
- Odor & Taste: Mild, characteristic cereal flavor
- Solubility: Moderate water dispersibility
- Particle Size: Customized according to customer requirements
- Moisture Content: Typically ≤8%
- Packaging Options:
- 20 kg multi-layer paper bags with PE liner
- 25 kg kraft paper bags
- 500 kg–1000 kg jumbo bags
- Shelf Life: 24 months when stored in a cool, dry, and sealed environment
3. Core Industrial Applications
Brown Rice Protein Concentrate is extensively utilized across multiple industrial sectors, including food processing, beverage manufacturing, sports nutrition, dietary supplements, infant and elderly nutrition formulations, bakery products, dairy alternatives, meal replacements, and functional health foods.
Its primary applications include protein fortification of beverages, plant-based meat products, nutritional powders, protein bars, breakfast cereals, baked goods, vegan dairy alternatives, and specialized nutritional formulations. Compared with many conventional protein ingredients, it offers excellent allergen-friendly characteristics, non-GMO compatibility, clean-label positioning, and superior consumer acceptance in plant-based formulations. Its consistent quality, long shelf life, and processing stability help manufacturers improve production efficiency while supporting premium product positioning.
4. Competitive Advantages
- Consistent protein quality supported by standardized manufacturing processes
- Reliable global supply with stable bulk production capacity
- Efficient international logistics supporting large-volume commercial shipments
- Competitive pricing for industrial-scale procurement and long-term supply contracts
- Sustainable plant-based ingredient with a lower environmental footprint than many animal-derived proteins
- Comprehensive technical documentation including COA, specification sheets, MSDS, and quality certificates available upon request
- Suitable for vegan, vegetarian, clean-label, and allergen-conscious product development
- Excellent batch-to-batch consistency for industrial manufacturing operations
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): Bulk 20 MT
- Loading Capacity: 20–24 MT per 20-ft container (depending on packaging configuration)


Reviews
There are no reviews yet.