Description
1. Product Overview
Berberine HCl 97% Powder is a high-purity botanical alkaloid ingredient derived from berberine-containing plants, standardized for use in nutraceutical, pharmaceutical, and dietary supplement manufacturing. It is primarily used in the formulation of capsules, tablets, functional supplements, and specialized health products. With a minimum berberine hydrochloride content of 97%, it offers manufacturers a concentrated, standardized ingredient for consistent formulation and quality control. Its strong demand in the global nutraceutical market makes it a commercially valuable ingredient for supplement producers and bulk ingredient distributors.
2. Key Specifications & Technical Characteristics
-
Product Code: BER-001
-
Chemical Composition: Berberine Hydrochloride (C₂₀H₁₈ClNO₄)
-
Purity: 97% minimum
-
Physical Form: Fine powder
-
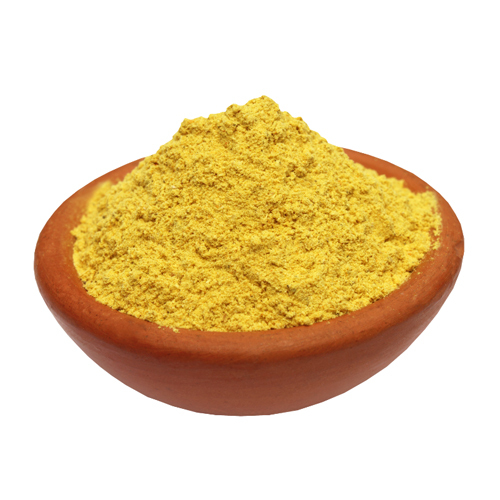
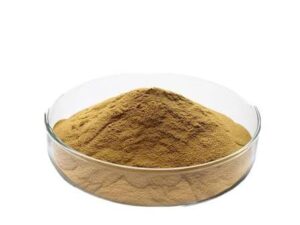
Appearance: Yellow to yellowish-green powder
-
Solubility: Soluble in water
-
Grade: Nutraceutical / Pharmaceutical ingredient grade
-
Particle Size: Customizable according to buyer requirements
-
Packaging: 1kg, 5kg, 25kg fibre drums or aluminium foil bags
-
Shelf Life: Typically 24 months under recommended storage conditions
-
Storage: Store in a cool, dry place, protected from light and moisture
-
Origin: Subject to supplier specification and batch documentation
3. Core Industrial Applications
-
Nutraceutical Manufacturing: Used as an active ingredient in dietary supplement capsules, tablets, and powder formulations.
-
Pharmaceutical Industry: Applied in the development and manufacturing of berberine-based pharmaceutical preparations, subject to applicable regulatory requirements.
-
Functional Nutrition: Incorporated into specialized wellness and functional health formulations.
-
Contract Manufacturing: Suitable for private-label supplement production and large-scale ingredient blending.
-
Bulk Ingredient Distribution: Supplied to nutraceutical wholesalers, ingredient importers, and international formulation companies.
Its standardized purity supports accurate ingredient dosing, formulation consistency, and efficient large-scale manufacturing compared with less concentrated botanical extracts.
4. Competitive Advantages
-
High-Purity Standardization: Minimum 97% berberine hydrochloride content supports consistent formulation and quality control.
-
Quality Consistency: Batch-specific testing and certificates of analysis support reliable procurement.
-
Supply Reliability: Bulk availability for commercial manufacturers, distributors, and international buyers.
-
Logistics Capability: Industrial packaging suitable for international freight and bulk ingredient shipments.
-
Price Competitiveness: Volume-based sourcing opportunities for wholesalers and large-scale manufacturers.
-
Technical Documentation: COA, MSDS/SDS, and relevant product specifications available subject to supplier confirmation.
-
Storage Efficiency: Stable powdered format with appropriate moisture-protective packaging.
5. Commercial & Supply Information
-
Minimum Order Quantity (MOQ): 20 Metric Tons (Bulk).
-
Bulk Loading Capacity: Subject to packaging configuration, container payload limits, and applicable shipping regulations.
-
Standard Container Options: 20FT and 40FT containers.
-
Supply Format: Bulk industrial supply.
-
Export Documentation: Commercial invoice, packing list, certificate of analysis, certificate of origin, and applicable shipping documentation, subject to availability.

Reviews
There are no reviews yet.