Description
1. Product Overview
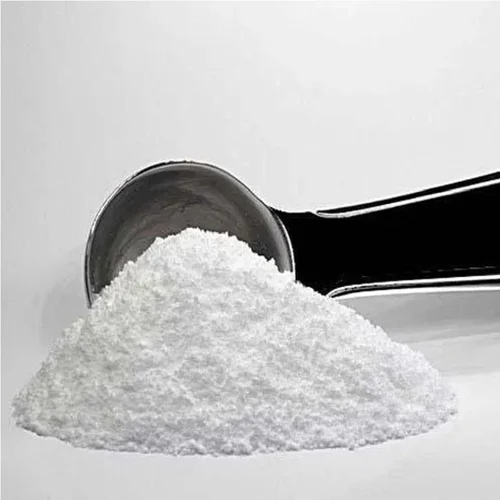
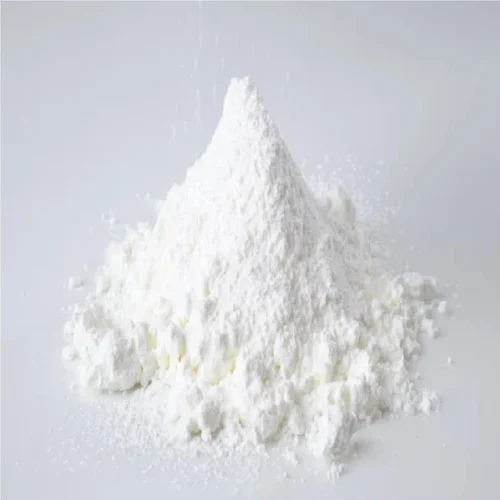
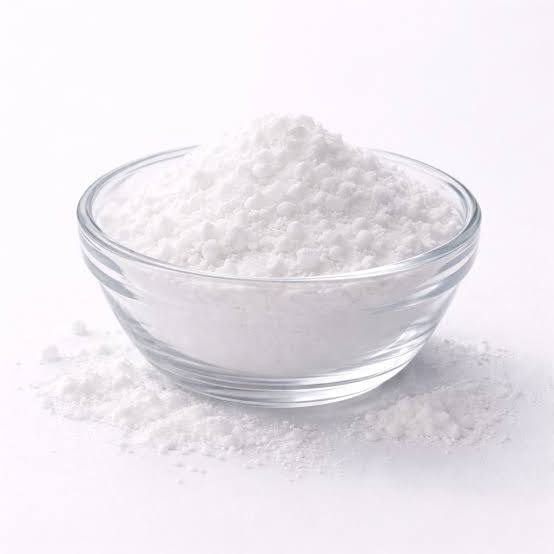
Natural Caffeine 98% Powder is a high-purity botanical-derived caffeine ingredient designed for commercial manufacturing and industrial formulation. It delivers concentrated stimulant functionality for energy drinks, dietary supplements, functional foods, sports nutrition, and pharmaceutical applications. Its high caffeine concentration enables precise dosage control, formulation efficiency, and consistent product performance. It serves as a strategic ingredient for manufacturers responding to growing global demand for energy-enhancing and performance-oriented products.
2. Key Specifications & Technical Characteristics
-
Chemical Composition: Naturally derived caffeine (C₈H₁₀N₄O₂).
-
Purity Level: 98% minimum caffeine content.
-
Physical Form: Fine crystalline powder.
-
Colour: White to off-white.
-
Odour: Odourless or nearly odourless.
-
Solubility: Soluble in hot water; limited solubility in cold water.
-
Packaging: 1kg, 5kg, 25kg fibre drums or aluminium foil bags.
-
Shelf Life: 24 months when stored under recommended conditions.
-
Storage: Keep sealed in a cool, dry place away from moisture and direct sunlight.
-
Origin: Subject to supplier and botanical extraction source.
3. Core Industrial Applications
-
Energy Drinks: Used in energy shots, carbonated energy beverages, and ready-to-drink formulations.
-
Dietary Supplements: Incorporated into caffeine capsules, tablets, powders, and stimulant blends.
-
Sports Nutrition: Used in pre-workout formulations and performance-oriented nutritional products.
-
Functional Foods: Applied in energy bars, fortified beverages, and functional confectionery.
-
Pharmaceutical Manufacturing: Used as an active ingredient in approved pharmaceutical formulations.
-
Nutraceutical Industry: Supports the production of concentrated energy and alertness formulations.
Its high purity supports accurate dosing, reduced ingredient loading, and consistent formulation performance compared with lower-concentration caffeine ingredients.
4. Competitive Advantages
-
High-Purity Composition: 98% caffeine concentration supports efficient industrial formulation.
-
Quality Consistency: Standardized specifications facilitate batch-to-batch formulation control.
-
Supply Reliability: Suitable for recurring procurement and large-volume manufacturing requirements.
-
Logistics Capability: Bulk packaging options support international shipping and commercial distribution.
-
Price Competitiveness: Concentrated composition offers efficient ingredient utilization.
-
Documentation: Certificate of Analysis (COA), Safety Data Sheet (SDS), and relevant quality documentation available subject to supplier verification.
-
Strategic Sourcing: Suitable for beverage manufacturers, supplement brands, nutraceutical producers, and international ingredient distributors.
5. Commercial & Supply Information
-
Minimum Order Quantity (MOQ): Bulk – 20 MT.
-
Loading Capacity: Approximately 20 MT per 20-foot container, subject to packaging configuration, gross weight limits, and shipping requirements.

Reviews
There are no reviews yet.